



Professional Thermal and Fluid Control Equipment
Optimizing engine longevity and hydraulic efficiency with precision-manufactured pumps designed for rigorous operational demands.

High Flexible Plum Type Elastic Coupling of All Size ML1 ML2 ML3 ML4 ML5 ML6 ML7 ML8 ML9

Reasonable price for 400cc Bm5/Oms/2K/2000/BMS/Hms Rectangle Splined Flange 27mm Flat Key Shaft Hydraulic Orbital Cycloid Motor
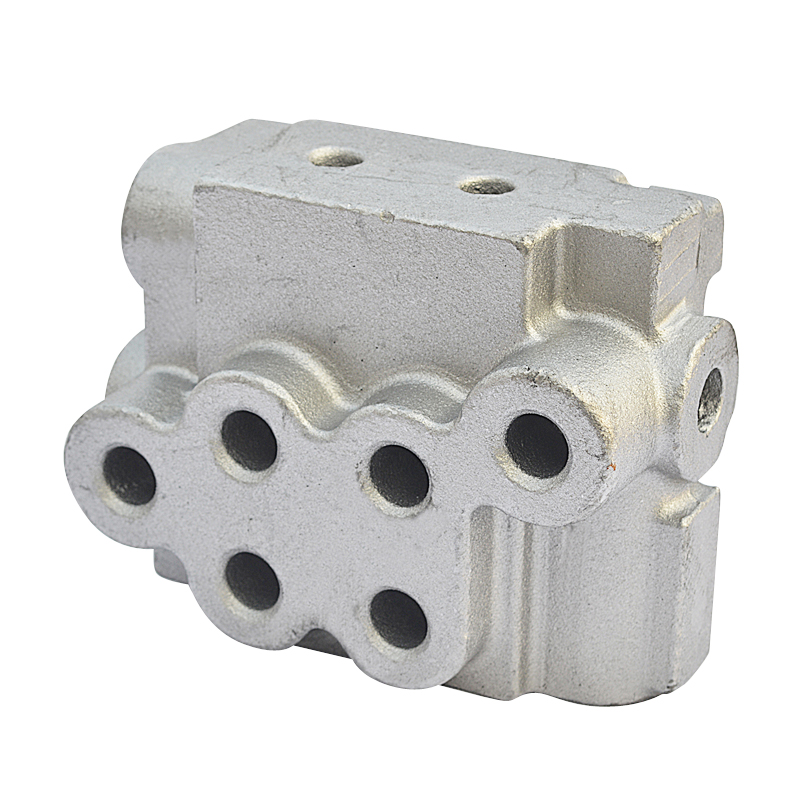
P40-2 Hydraulic multi-way valve castings
Addressing the critical need for efficient cooling in high-temperature environments.
In the harsh climatic conditions of Kuwait, where ambient temperatures frequently exceed 45°C, the reliability of an engine cooling pump is not just a matter of efficiency, but of operational survival. Heavy machinery used in oil extraction, construction, and logistics faces severe thermal stress, making high-flow, heat-resistant cooling systems a priority for local fleet managers and industrial operators.
The prevalence of heavy-duty diesel engines across the region increases the demand for specialized components like the oil engine water pump. Local businesses often struggle with premature component failure due to dust ingress and overheating. Consequently, there is a shifting preference toward "Euro-standard" precision parts that offer tighter tolerances and better material durability against corrosive environmental factors.
As Kuwait continues to invest in infrastructure and petrochemical expansion, the integration of high-capacity engine cooling water pump systems is becoming essential. There is a growing opportunity for suppliers who can provide integrated R&D and customized manufacturing, ensuring that hydraulic and cooling components are perfectly matched to the specific load profiles of equipment operating in the Arabian Peninsula.
Evolution of Fluid Power and Cooling Technology
Tracing the trajectory from basic mechanical pumps to precision hydraulic systems.
Industry Development Path
Early Stage
Mechanical Standardization
Focus on basic cast-iron gear pumps and water pumps with standard tolerances for general agricultural and industrial use.
Growth Era
Precision Engineering
Introduction of aluminum alloys and NBR seals to improve weight-to-power ratios and chemical resistance in hydraulic systems.
Modern Era
Customized Integration
Shift toward OEM-specific designs and computer-controlled testing to meet strict international emission and efficiency standards.
Emerging Technical Trends
- Material Innovation Implementation of high-strength composites to reduce wear and tear in sandy environments.
- Intelligent Monitoring Integration of sensors to track flow rates and temperatures in real-time for predictive maintenance.
- Energy Efficiency Redesigning pump geometries to reduce parasitic loss, directly lowering fuel consumption for heavy machinery.
Strategic Directions in Pump Manufacturing
Analyzing the technical and commercial shifts impacting the global supply chain.
Manufacturing Automation
The use of flexible machining centers and computer-controlled testing ensures that every pump meets exact OEM specifications with zero variance.
Climate-Adaptive Design
Developing specialized seals and alloys that resist thermal expansion and contamination, specifically for Middle Eastern operational contexts.
Supply Chain Resilience
Moving toward a "one-shop" integration model where R&D, manufacturing, and trade are centralized to reduce lead times and costs.
Standardization
Adopting global benchmarks such as GOST and GSTU for mounting flanges and shafts to ensure cross-brand compatibility.
The long-term commercial value in this sector lies in the transition from selling a "component" to providing a "thermal solution." As engines become more powerful and compact, the ability to dissipate heat more effectively becomes a primary competitive advantage for machinery manufacturers.
Local procurement in Kuwait is increasingly favoring manufacturers who can offer technical support and rapid delivery of critical spares. The shift toward integrated service centers—combining supply chain management with technical expertise—is defining the new industry standard.
Industrial Application Across Kuwait
Integrating high-precision pump technology into the region's most critical operational environments.
1
Oil Field Infrastructure
In oil extraction sites, heavy-duty drilling rigs rely on excavator gear pump systems to maintain hydraulic pressure for lifting and rotation under extreme heat.
2
Road & Bridge Construction
Concrete pump trucks and pavers operating in Kuwait's urban expansion projects require consistent flow from auxiliary pumps to prevent engine overheating during midday peaks.
3
Port & Marine Logistics
Ship deck machinery and rudder control systems utilize high-pressure hydraulic motors and pumps to manage heavy loads in salt-heavy, humid coastal air.
4
Mining & Quarrying
Heavy excavators and dozers in desert quarries use reinforced gear pumps to ensure walking and swing motors operate smoothly despite high dust concentration.
5
Agricultural Equipment
Modern irrigation and farming machinery in Kuwait's greening projects depend on euro water pump standards for fuel efficiency and lower maintenance.
Brand Story
The global development journey of Hebei Longshengtengyu Pump Industry Co., Ltd.
2000
Company Foundation
Established as a dedicated industrial water pump manufacturer in China, focusing on the core principles of power, quality, and efficient service.
2010
Technological Expansion
Integrated R&D with manufacturing, developing a specialized team with over a decade of expertise in hydraulic design and processing.
2015
Certification & Patents
Secured numerous hydraulic utility model patents and established its own brand trademark, enhancing global market competitiveness.
2018
Advanced Equipment Upgrade
Implemented flexible machining centers and CAT computer-controlled testing machines to guarantee high-precision production.
2020
Global Market Reach
Successfully expanded exports to Russia, Belarus, the Czech Republic, and the Middle East, satisfying diverse international standards.
Present
Comprehensive Integration
Operates four specialized centers—Marketing, Supply Chain, Manufacturing, and Integration—to provide total water and hydraulic solutions.
High-Performance Hydraulic and Cooling Components
Explore our comprehensive range of gear pumps and water pumps engineered for durability and maximum flow efficiency.

DCV series of DCV40,DCV60,DCV100,DCV140,DCV200 sectional hydraulic manual directional control valve

98497117 98465322 FIAT water pump

CBK Series Aluminium alloy Cbk1-f0.63 Cbk1-f1.2 Cbk1-f1.6 Cbk1-f0.8 Cbk1-f2.1 Hydraulic Gear Pump

Replace Parker hydraulic gear pump PGP PGM Series Hydraulic Gear Pump PGP620 PGP640 PGP315 PGP500 PGP502 PGP505 PGP511 PGP517
Technical Support and Procurement FAQ
Detailed answers to common technical and commercial queries regarding our pump systems.
What are the technical specifications for gear pumps used in excavator applications?
Our gear pumps, such as the PGP series, feature fixed displacement designs with high-strength aluminum alloy bodies and NBR or Viton seals to ensure durability. Specific displacement and pressure ratings are matched to the machine's hydraulic requirements.
How do I ensure the engine cooling pump is compatible with my existing system in Kuwait?
Compatibility is ensured by verifying the mounting flange and shaft dimensions. We follow GSTU and GOST standards, and our technical team can provide customized adaptations based on your specific OEM model number.
What manufacturing quality controls are implemented for the water pumps?
We utilize flexible machining centers and CAT computer-controlled testing machines. Every pump undergoes rigorous pressure and flow testing to ensure it meets industry standards before leaving our facility.
Can you provide customized hydraulic gear pumps for non-standard machinery?
Yes, we integrate R&D and manufacture into one process, allowing us to develop customized products based on your technical drawings or performance requirements for specialized industrial equipment.
What is the recommended maintenance cycle for pumps operating in high-dust environments?
In desert conditions, we recommend more frequent seal inspections and fluid filtration checks. Using high-quality NBR or Viton seals can extend the lifespan by preventing premature wear from abrasive particulates.
What are the commercial terms and lead times for bulk orders to Kuwait?
We offer reasonable payment terms and fast delivery through our dedicated supply chain management center. Minimum order quantities typically start at 50 pieces, with a monthly supply capacity of up to 10,000 pieces.
Secure Your Equipment's Thermal Reliability Today
Partner with Hebei Longshengtengyu to access professional-grade hydraulic and cooling solutions tailored for the Kuwaiti market. Benefit from 21 years of manufacturing excellence and a streamlined global supply chain.
Request Technical Quote


 English
 Afrikaans
 Arabic
 Belarusian
 Bulgarian
 Esperanto
 French
 German
 Kazakh
 Polish
 Portuguese
 Romanian
 Russian
 Spanish
 Tajik
 Turkish
 Turkmen
 Ukrainian
 Uzbek
 Vietnamese