



Precision Cooling and Hydraulic Pump Systems
Reliable fluid management components designed for construction, agriculture, and industrial applications.
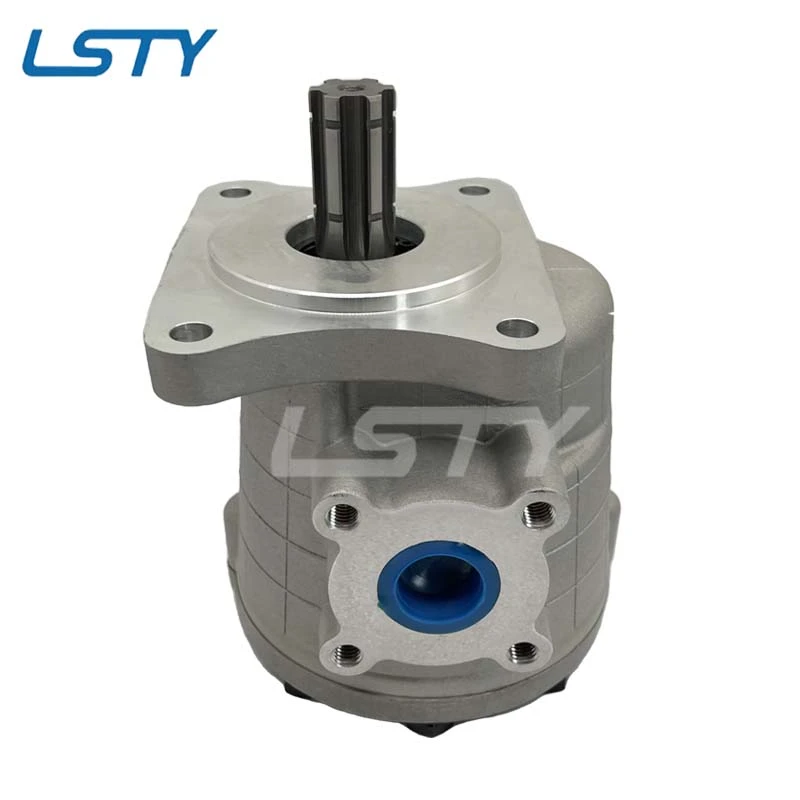
NSH Gear Pump NSH 50A-3L(Насос шестеренный НШ 50А НШ 50А-3Л)
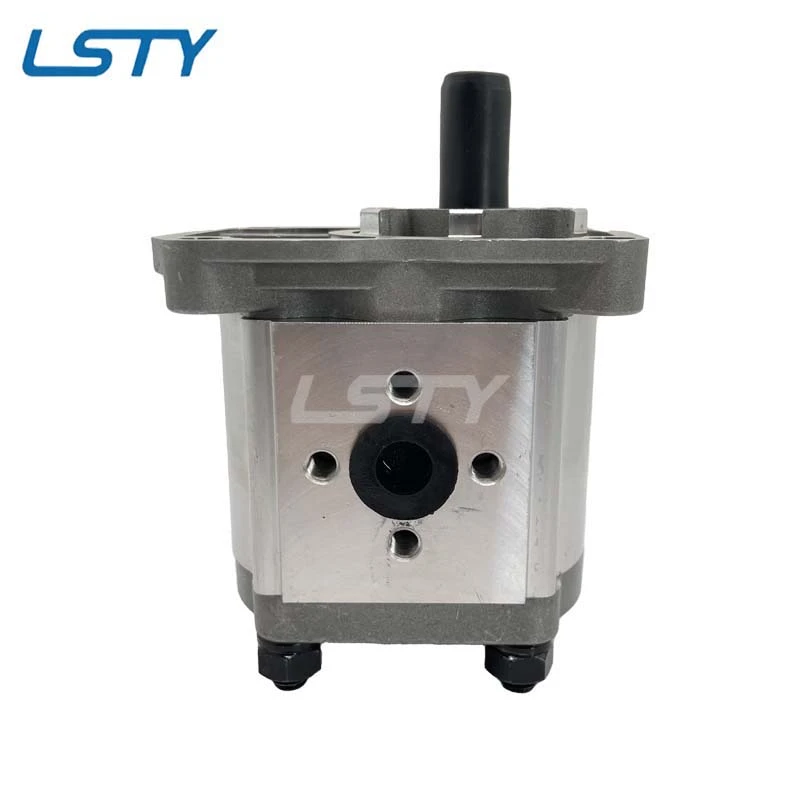
Насос шестеренчатый НШ14М-3 правый Gear Pump NSH14M-3
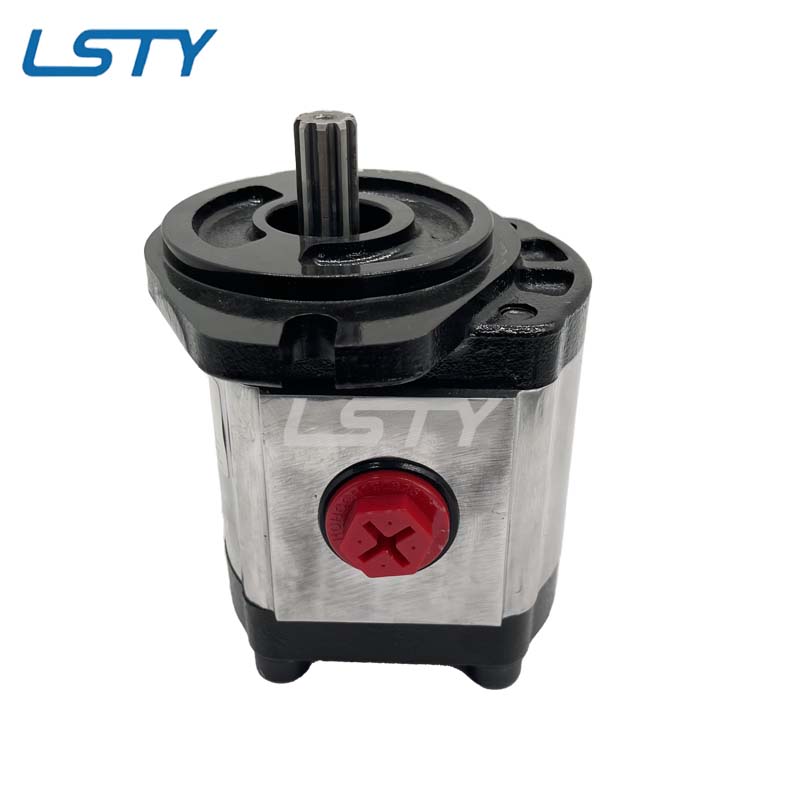
high performance and high power Parker Aluminum Pump PGP500 PGP511 PGP517 Series fixed displacement gear pump for Agriculture Machinery
Analyzing Pump Requirement Trends in Austria
Adapting hydraulic and cooling technology to the specific industrial landscape of Central Europe.
Austria's industrial sector, characterized by high-precision engineering and a strong focus on sustainable machinery, requires fluid components that can withstand varied Alpine climatic conditions. The demand for a reliable engine cooling pump is driven by the need for thermal stability in heavy-duty equipment operating in both high-altitude and urban environments.
Local procurement trends indicate a shift toward integrated hydraulic systems that prioritize energy efficiency and reduced downtime. For construction and forestry equipment, the selection of an excavator gear pump now focuses on high volumetric efficiency and compatibility with modern European emission standards, ensuring seamless integration into existing fleets.
Operational challenges in the region often center on maintenance accessibility and the longevity of seals under extreme pressure. Austrian operators increasingly seek "one-stop" solutions that combine the supply of an oil engine water pump with professional technical support to optimize the lifecycle of their industrial assets.
Evolution of Industrial Pump Technology
From basic fluid displacement to intelligent, high-efficiency thermal management.
Market Development History
-
Early Adoption Stage
Focus on basic cast-iron pump designs for simple water circulation and hydraulic lifting in early industrial machinery. -
Standardization Stage
Introduction of universal mounting flanges and standardized gear ratios, improving the interchangeability of the euro water pump across different European brands. -
Integration Stage
Current shift toward using lightweight alloys and precision-machined internals to maximize flow rates while reducing overall system weight.
Future Development Trends
- Predictive Maintenance — Transitioning from scheduled replacements to sensor-based monitoring of pump wear and pressure drops.
- Energy Efficiency — Development of variable displacement pumps to reduce parasitic power loss in engine cooling systems.
- Material Sustainability — Increased use of high-strength, recyclable composites to replace traditional heavy metal housings without sacrificing durability.
Strategic Outlook for Fluid Power Systems
Key drivers shaping the next generation of engine cooling and hydraulic pumping.
Precision Manufacturing
Utilization of flexible machining centers to achieve micron-level tolerances in gear pumps, reducing internal leakage.
Thermal Optimization
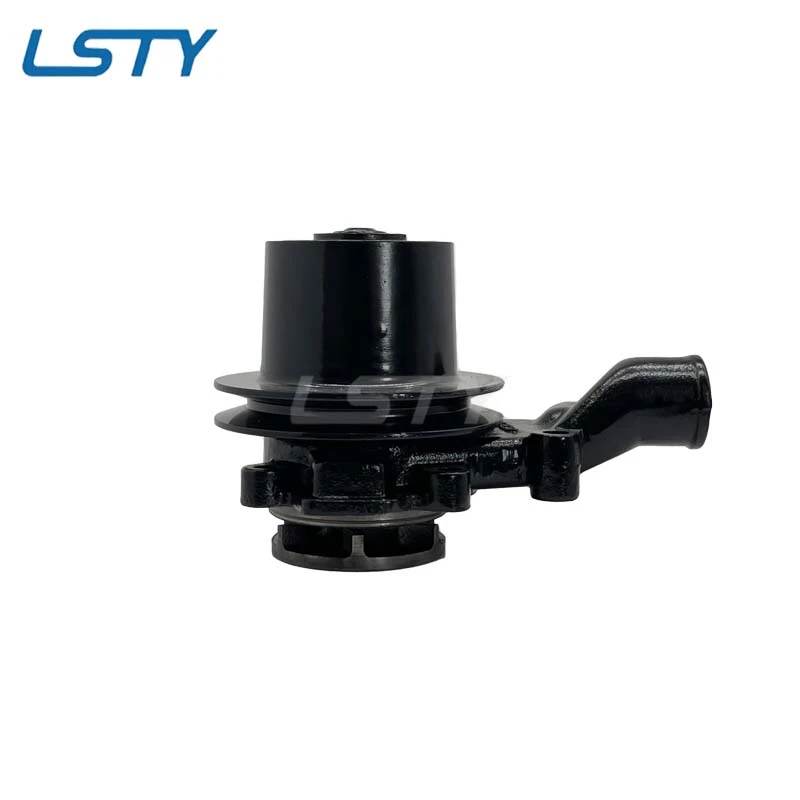
Advanced impeller designs in the engine cooling water pump to maximize heat dissipation in compact engine bays.
Modular Compatibility
Designing pump interfaces that allow for rapid swapping between different power units without modifying the chassis.
Supply Chain Agility
Implementing integrated supply chain centers to ensure fast delivery of critical pump components to European job sites.
Future Industrial Outlook
Over the next 3-5 years, the Austrian machinery market will likely see a stronger convergence of hydraulic power and electronic control. This evolution will require pumps that are not only mechanically robust but also capable of operating within highly modulated systems to save fuel and reduce emissions.
From a commercial perspective, the ability to provide customized pump specifications—rather than generic off-the-shelf parts—will become a key competitive advantage for manufacturers supporting the region's specialized agricultural and construction sectors.
Industrial Application Scenarios in Austria
Practical implementations of high-performance pumping technology across diverse sectors.
1
Alpine Infrastructure Construction
Utilizing heavy-duty gear pumps in excavators and pavers for road building in mountainous terrain, where high torque and reliable cooling are essential for steep inclines.
2
Agricultural Machinery Fleet
Implementing specialized water pumps in combine harvesters and tractors to ensure engine stability during intensive harvesting seasons in rural Austrian provinces.
3
Municipal Concrete Operations
Applying high-pressure auxiliary pumps in concrete mixer trucks and pump trucks for urban development projects in Vienna and Graz.
4
Specialized Mining Equipment
Deploying reinforced hydraulic pumps for drilling and extraction machinery used in regional mineral deposits, focusing on wear resistance in abrasive environments.
5
Marine and Port Hydraulics
Integrating deck machinery pumps and control systems for river barge operations along the Danube, ensuring corrosion-resistant fluid transport.
Engineering Excellence: HEBEI LONGSHENGTENGYU PUMP INDUSTRY CO., LTD
Two decades of commitment to hydraulic innovation and industrial fluid solutions.
00
2000
Company Foundation
Established as a dedicated industrial water pump manufacturer in China, focusing on integrating R&D and manufacturing to provide efficient fluid solutions.
10+
Expertise Development
Hydraulic Specialization
Our technical teams accumulated over 10 years of deep experience in the hydraulic field, specializing in the design and machining of professional gear pumps.
21
21 Years of Growth
Global Market Expansion
Developed a robust portfolio including 20 hydraulic utility model patents, exporting high-quality pumps to Russia, Belarus, Czech Republic, and the Middle East.
Hydraulic and Cooling Solutions for Austrian Industry
A comprehensive range of gear pumps, water pumps, and custom hydraulic fittings engineered to industry standards.
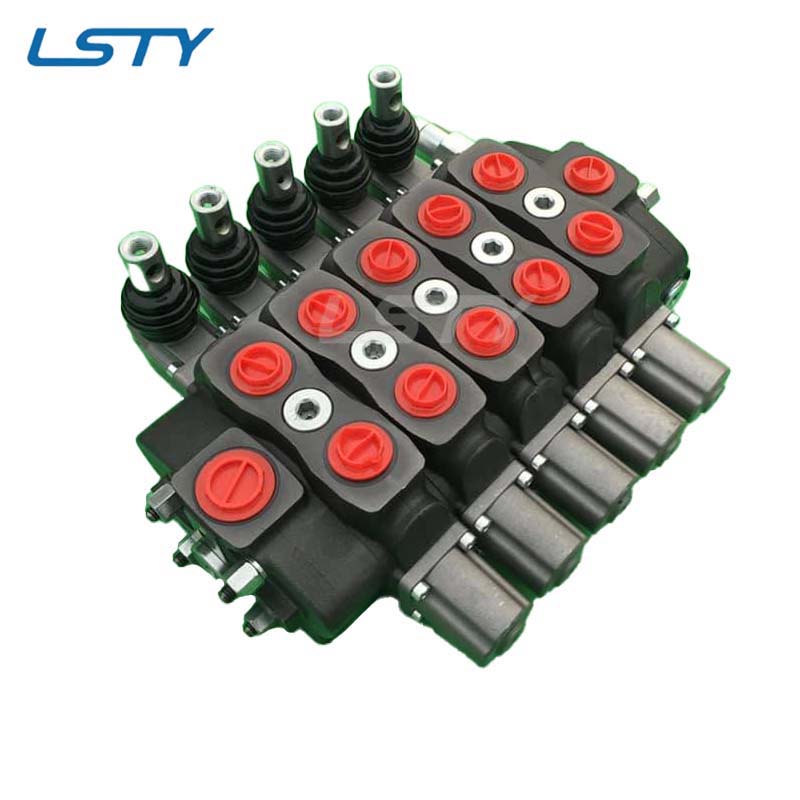
SD25 Series hydraulic Directional Valve 1-12spools Directional Control Valve Hydraulic Sectional Control Valve
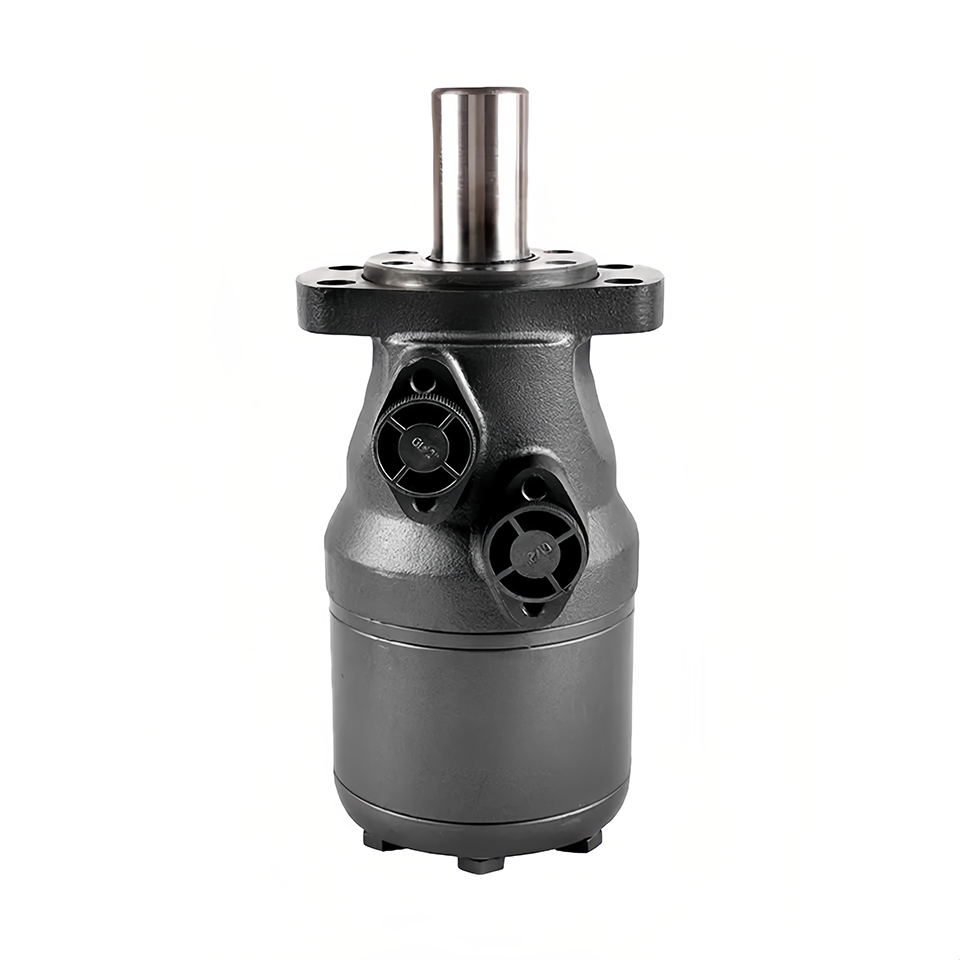
BMH/OMH Series Cycloid Hydraulic Motor,BMH-200 BMH-250 BMH-315 BMH-400 BMH-500
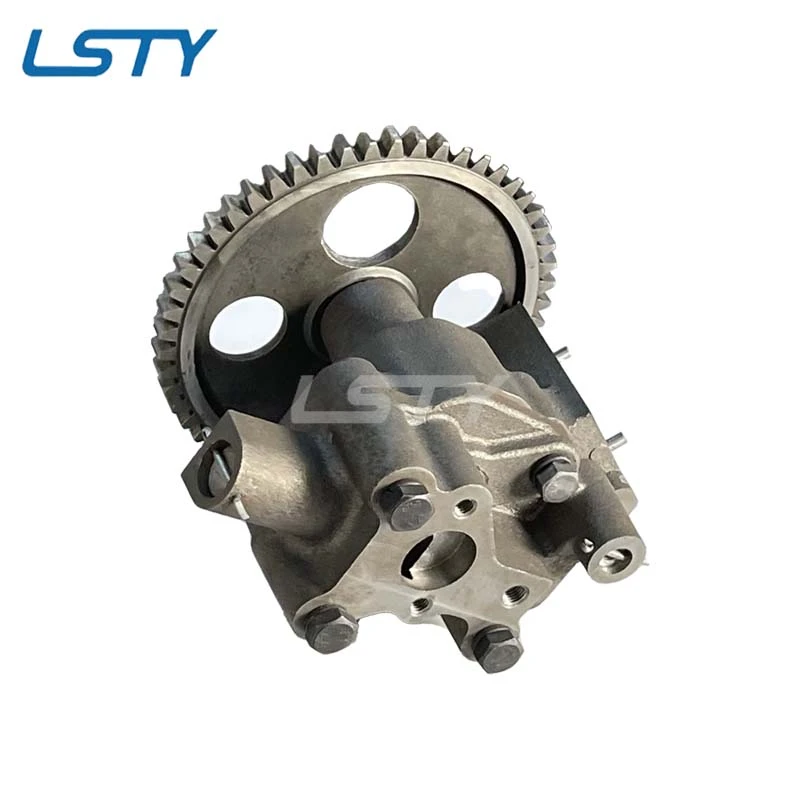
740.60-1011010 Oil pump KAMAZ-EURO-3
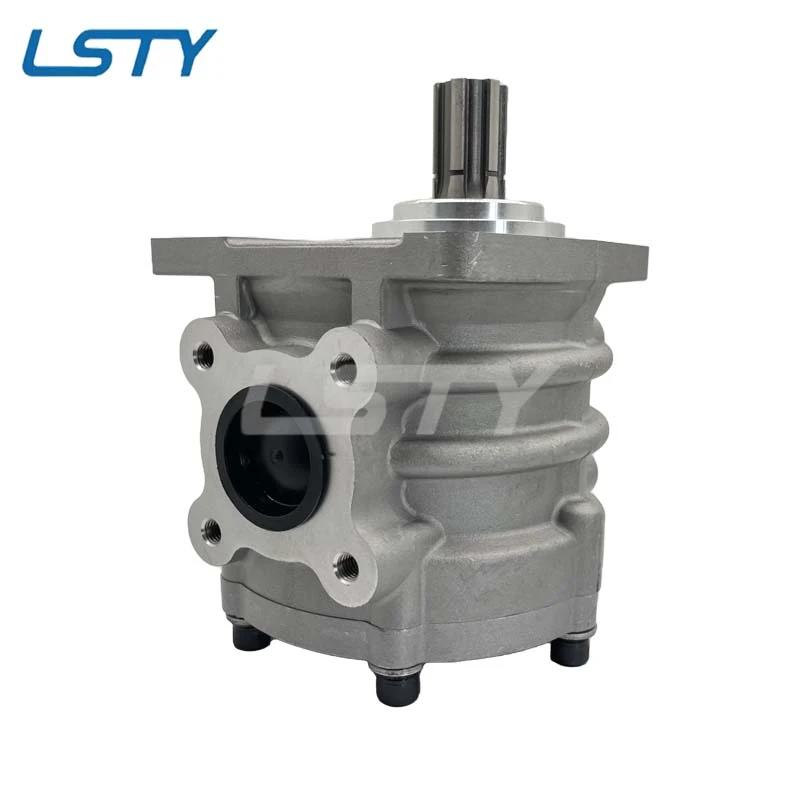
Nsh100A Pump MTZ Hydraulic Gear Pump Elevator Pump for Wheeled Tractor Bulldozers NSH100A-3L
Technical FAQ for Pump Procurement in Austria
Expert answers to common queries regarding selection, installation, and maintenance.
How do I select the correct engine cooling pump for high-altitude operation in the Alps?
Selection should focus on the pump's flow capacity and the impeller's efficiency at lower atmospheric pressures. We recommend analyzing the maximum engine thermal load and ensuring the pump can maintain consistent coolant circulation without cavitation under varying altitude conditions.
What are the main advantages of using a hydraulic gear pump for construction equipment?
Gear pumps offer high reliability, a compact design, and the ability to handle high-viscosity fluids. They are ideal for excavator and paver systems due to their durability and relatively simple maintenance requirements compared to piston pumps.
Are your euro water pumps compatible with standard European engine mounts?
Yes, our products are manufactured according to strict industry standards. We provide various flange and shaft configurations to ensure compatibility with widely used European engine specifications, reducing the need for modifications during installation.
What is the typical lead time for customized pump orders to Austria?
Lead times depend on the complexity of the customization and the order volume. However, we utilize a well-managed supply chain and manufacturing center to offer reasonable delivery schedules and efficient shipping to the European region.
How can I prevent premature wear in an oil engine water pump?
The most effective method is maintaining the purity of the coolant and ensuring that the system is properly bled of air. Using high-quality seals (such as Viton where available) and following the manufacturer's lubrication intervals will significantly extend the pump's operational life.
Does HEBEI LONGSHENGTENGYU provide technical support for onsite installation?
Yes, our business scope includes on-site support, repairing, and reconditioning. Our experienced technical team can provide guidance on product integration and operational optimization to ensure your systems perform at peak efficiency.
Optimize Your Machinery's Fluid Systems
Discuss your specific technical requirements and project goals for the Austrian market with our engineering team today.
Contact Us Now


 English
 Afrikaans
 Arabic
 Belarusian
 Bulgarian
 Esperanto
 French
 German
 Kazakh
 Polish
 Portuguese
 Romanian
 Russian
 Spanish
 Tajik
 Turkish
 Turkmen
 Ukrainian
 Uzbek
 Vietnamese